
CRYOGENIC TECHNOLOGY,
LEADING THE FUTURE
Efficient and energy-saving cryogenic solutions ensuring product quality and safety across industries.
This page is not the official website. Generated by AI, does not constitute any advice. If needed, please click here to visit the corresponding official website.
Efficient and energy-saving cryogenic solutions ensuring product quality and safety across industries.
Precision monitoring protects every valuable item with real-time temperature control and fail-safe systems.
Our advanced insulation and flow systems reduce boil-off and energy consumption by up to 30%.
Innovative solutions for ultra-low temperature applications in research, healthcare, and clean energy.
Comprehensive cryogenic solutions for storage, transfer, protection, and application across industries.
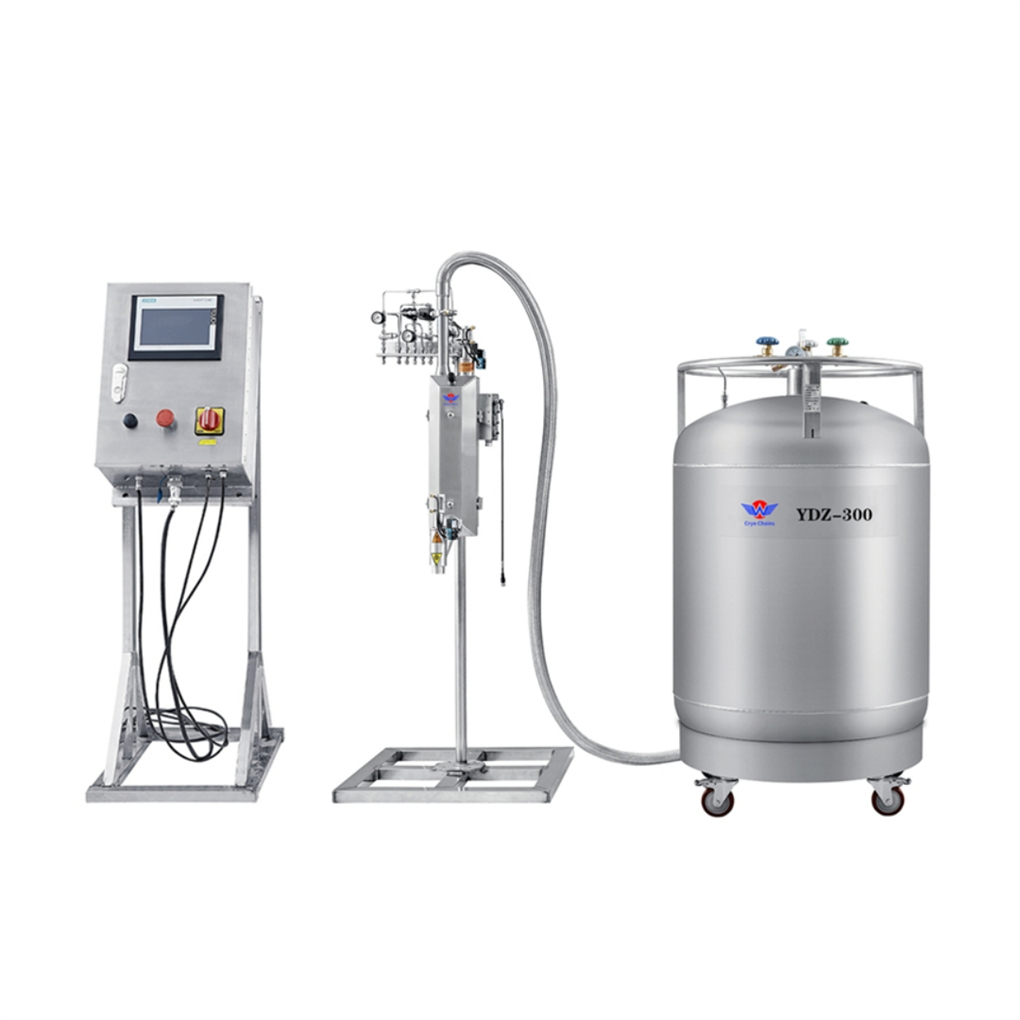
Precision dispensing for food freezing, medical, and industrial applications.

Valves, dewars, and transport systems for ultra-low temperature research.

High-efficiency vacuum-insulated tanks for LN2, LH2, and LHe.
Full-body protection against extreme cold with enhanced mobility.

Leak-proof, low-heat-leak pipelines for safe cryogenic transfer.
Whole-body cryotherapy systems for sports recovery and wellness.
High-throughput freezing for food processing with precise control.
Safe, long-duration transport of biological samples without liquid.
WOBO Industrial Group Cryochains is a leading provider of advanced cryogenic and energy solutions, serving over 100 countries across diverse industries such as new energy, metallurgy, and petrochemicals.
With a dedicated team of more than 200 skilled professionals and over 15 years of production experience, we leverage cutting-edge technologies and strict quality control to ensure excellence in every product. Our 50,000+ square foot manufacturing facility is equipped for innovation and scalability.
Countries Served
Years Experience
Sq Ft Production Area
Employees
Tailored cryogenic systems for biobanks, food processing, energy, and research.
Complete sample storage and logistics with LN2 vapor-phase systems and monitoring.
Bulk storage and distribution systems for hospitals, labs, and industrial sites.
Custom vacuum-insulated pipeline networks for safe, efficient transfer.
Tunnel and spiral freezers using liquid nitrogen for rapid, high-quality freezing.
Precision dosing for temperature control in food, pharma, and chemical processes.
Storage, transport, and refueling systems for clean energy applications.
Our core advantages ensure reliability, innovation, and global support.
Products sold in over 100 countries with proven performance in extreme environments.
Over 15 years of specialized production and engineering in cryogenics.
ISO-certified manufacturing with rigorous testing and traceability.
Custom engineering and responsive support to meet unique application needs.
We provide equipment for liquid nitrogen (LN2), liquid helium (LHe), and liquid hydrogen (LH2), with specialized systems for each.
Yes, our engineering team designs custom storage, transfer, and application systems based on client specifications.
We serve biobanks, food processing, healthcare, aerospace, clean energy, and research institutions globally.
Yes, all cryogenic protective gear meets international safety standards including EN 511 and ASTM F1702.
For inquiries, quotes, or technical support, visit our official website.
Phone: +86 131 4059 0596
Email: [email protected]
Notice for Buyers: If you are a buyer, the above information is generated by AI collection and does not constitute any advice. If necessary, please visit the corresponding official website.
For Domain Owners: If you are the domain owner and do not want to be included by fobcompany.info, please contact [email protected] via your corporate email to cancel. We will cancel your inclusion within 3 business days.
如果您是域名所有者 不想被fobcompany.info收录 请用企业邮箱联系[email protected] 取消收录 我们将在3个工作日取消您的收录
Service Request: If you are other domain and want to be included, please contact [email protected]
如果您是其他域名合作 也请联系[email protected]