This page is not the official website. Generated by AI, does not constitute any advice. If needed, please click here to visit the corresponding official website.
High-efficiency coal, biomass, oil & gas fired boilers, pulverized coal systems, and waste-to-energy incinerators engineered for performance, reliability, and environmental compliance.
As a leading provider in the thermal energy sector, industry-boiler.com represents cutting-edge boiler technology developed by Taishan Group. With decades of engineering excellence, we deliver robust, energy-efficient solutions for power generation, manufacturing, heating, and waste-to-energy applications across global industries.
Our product line includes coal-fired, biomass, oil & gas boilers, pulverized coal systems, and municipal solid waste incinerators — all designed with advanced combustion technologies, low emissions, and high thermal efficiency in mind.
Engineered for efficiency, durability, and environmental compliance — our industrial boiler systems meet the highest global standards.
Three-pass full wet back structure with large furnace and thick smoke pipe. Features threaded and corrugated furnace for enhanced heat transfer and fuel savings.
D-type arrangement, double-drum water tube boiler with full membrane wall structure and slightly positive pressure combustion.
Chain grate boiler for wood chips, biomass pellets. Double drum natural circulation with O-shaped arrangement.
Horizontal reciprocating grate boiler with 15° incline. Prevents ash slagging with cooling tubes at furnace outlet.
Circulating Fluidized Bed boiler for wood chips, bagasse, straw, rice husk. Energy-saving and low-emission design.
Double drum chain grate boiler with high heat efficiency and low coal leakage. Ideal for medium-pressure steam.
Double drum horizontal chain grate bulk boiler with air preheater. Stable and economical operation.
Single drum horizontal chain grate boiler. Designed for efficient and safe operation with full automation.
Complete system including coal storage, burner, control, flue gas purification, and fly ash recovery.
Third-generation energy-saving boiler with lime desulfurization and bag filter for clean emissions.
Municipal solid waste incineration for harmlessness, volume reduction, and energy recovery.
Delivered and installed in Cambodia. Proven performance in international markets.
Our industrial boiler systems combine innovation, reliability, and environmental responsibility.
Low NOx, low emissions, and advanced flue gas treatment systems ensure compliance with global environmental standards.
Optimized combustion, membrane walls, and heat recovery systems deliver thermal efficiency above 90%.
PLC & DCS control systems, remote monitoring, and predictive maintenance for seamless operation.
From Cambodia to Southeast Asia, our boilers power industries worldwide.
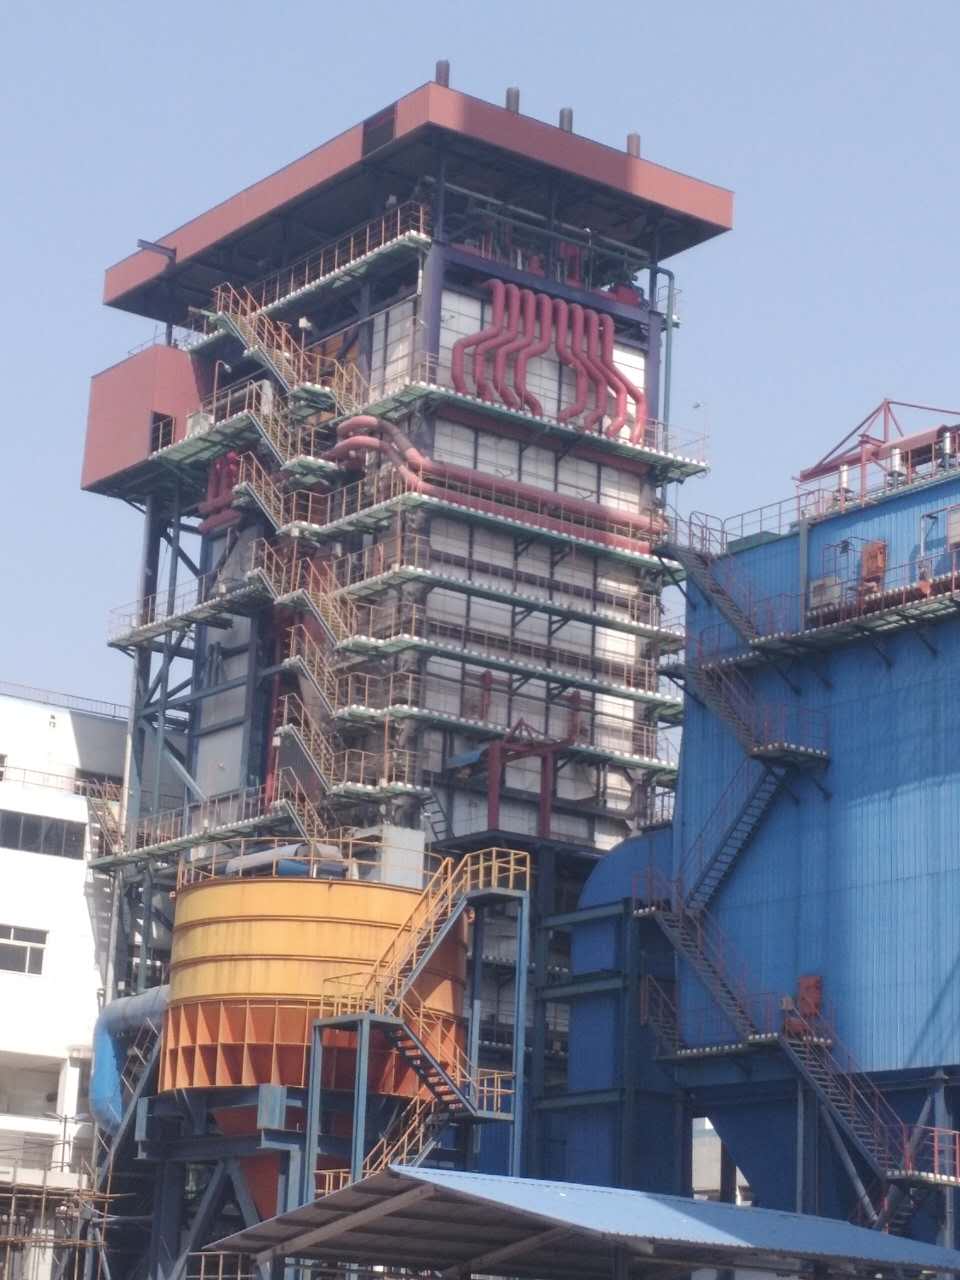
130TPH chain grate boiler delivered and commissioned for industrial steam supply.
Advanced circulating fluidized bed boiler undergoing drying and commissioning.
For product inquiries, technical support, or project collaboration, visit our official website to connect with our team.
Visit Official WebsiteNotice for Buyers: If you are a buyer, the above information is generated by AI collection and does not constitute any advice. If necessary, please visit the corresponding official website.
For Domain Owners: If you are the domain owner and do not want to be included by fobcompany.info, please contact [email protected] via your corporate email to cancel. We will cancel your inclusion within 3 business days.
如果您是域名所有者 不想被fobcompany.info收录 请用企业邮箱联系[email protected] 取消收录 我们将在3个工作日取消您的收录
Service Request: If you are other domain and want to be included, please contact [email protected]
如果您是其他域名合作 也请联系[email protected]